ER4047 aluminum welding wire, also known as "718 aluminum" or AlSi12, is a eutectic aluminum-silicon alloy with a silicon content of approximately 12%. Its low melting point and narrow solidification range provide excellent fluidity and wettability during welding, significantly reducing hot cracking and increasing weld shear strength.
Instant QuoteWithin Chalco's aluminum welding filler metal range, ER4047 is available for compatible MIG/GMAW and TIG/GTAW welding applications involving selected aluminum alloys. Filler selection depends on the base alloy, joint requirements, and welding procedure. Its high-silicon composition is also relevant to certain aluminum brazing filler materials, although brazing products differ from ER4047 welding wire in form and application.
ER4047 Aluminum Welding Wire Specifications and Packaging
| Item | Parameter range |
| Diameter (mm) | Wire coil: 0.60* / 0.80 / 0.90 / 1.00 / 1.20 / 1.60 / 2.00 / 2.40 |
| Straight strip: 1.20 / 1.60 / 2.40 / 3.20 / 4.00 / 5.00 / 6.00 | |
| Packaging form / Net weight | S100 0.5 kg|S200 2 kg|S300 5–7 kg|S360 20 kg|Drum 150 kg |
| Straight strips: 1000 mm long, 5–10 kg/box | |
| Wire diameter tolerance / Status | ±0.02 mm (ISO 544 h9) |
| Welding process | GTAW / TIG (straight strip) |
| GMAW / MIG (coiled wire) | |
| Recommended shielding gas | 100% Ar or Ar + ≤30% He (thick parts/high thermal conductivity substrate) |
| Implementation standard / Brand | AWS A5.10 ER4047 | AMS 4185 | ISO 18273 S Al 4047 |
| Applicable parent material | 1xxx, 3xxx, 6xxx, 7005 and 5xxx with Mg ≤3% |
| Minimum order quantity / Delivery | Minimum order for S100 0.5 kg or TIG 1 kg |
| Conventional stock shipped within 72 hours | |
| Technical support | Free welding parameter window, sample evaluation, COA/COC report and RoHS documents are provided |
Product Categories of ER4047 Aluminum Welding Wire
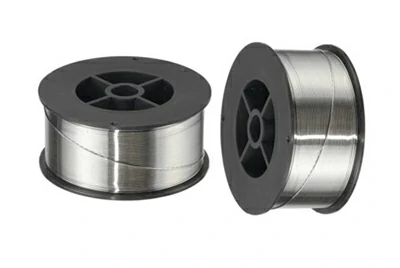
ER4047 MIG wire
Suitable for GMAW applications, this ER4047 grade is supplied as aluminum MIG welding wire in spool form for compatible automotive, industrial, and general manufacturing applications.
Type: Spool
Standard: AWS A5.10, ER4047
ER4047 TIG rod
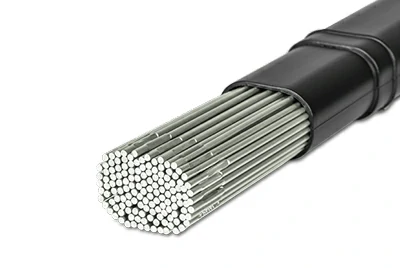
Suitable for Gas Tungsten Arc Welding (GTAW) processes, ideal for applications requiring high welding quality, such as precision manufacturing and repair.
Type: Straight
Standard: AWS A5.10, ER4047
ER4047 Flux Cored Wire
ER4047 flux-cored aluminum brazing filler is intended for suitable aluminum brazing applications where flux is incorporated into the filler material. Typical applications may include compatible HVAC aluminum return bends, manifolds, and tube assemblies.
Chalco provides ER4047 welding filler materials in different supply forms for suitable MIG and TIG applications. For projects using a brazing rather than fusion welding process, our aluminum brazing rods offer an additional product category to consider. Please share the required joining process, alloy grade, dimensions, and order quantity for product selection and quotation.
Instant QuoteFeatures of ER4047 Aluminum Welding Wire
ER4047 aluminum alloy is a high-silicon aluminum alloy (Si content 11–13%). This high silicon content gives it a low melting point and a narrow solidification range, resulting in excellent fluidity and crack resistance during welding/brazing. Its key alloy characteristics include:
- Excellent Welding Fluidity: The high silicon content (11–13%) enhances the fluidity of the molten weld pool, reducing porosity and lack of fusion, and achieving a smoother weld surface.
- Low Melting Point and Narrow Solidification Temperature Range: Its lower melting point (liquidus line approximately 577–582°C) and narrow solidification range minimize thermal stress concentration and post-weld deformation, effectively inhibiting hot cracking.
- Reduced Shrinkage: The high silicon content reduces the volume shrinkage of the alloy during solidification, improving the dimensional accuracy of welded parts and the strength of joints.
- Good High-Temperature Performance: It maintains stable performance in high-temperature environments and exhibits strong resistance to thermal fatigue and creep, making it suitable for applications such as heat exchangers and engine components.
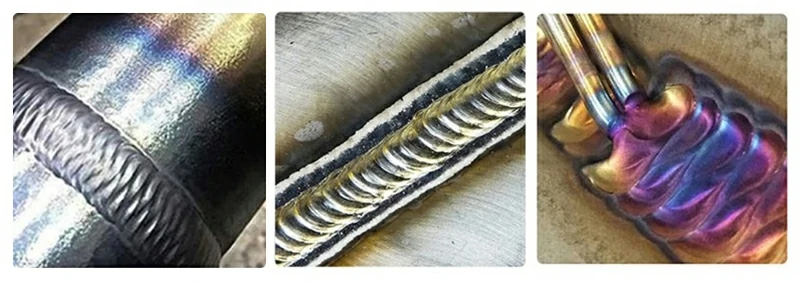
- Aesthetic Welds: It can form bright, virtually soot-free weld surfaces, eliminating the need for subsequent grinding or cleaning processes.
- Significantly Reduced Hot Cracking Sensitivity: When welding base materials sensitive to hot cracking (such as the 6xxx series), using ER4047 filler can significantly reduce crack formation, ensuring weld integrity.
- Excellent Corrosion Resistance and Thermal Conductivity: It has good resistance to atmospheric and humid heat corrosion and is not prone to oxidation. Its thermal conductivity is approximately 130 W/m·K, meeting the application requirements for heat exchange and electronic heat dissipation.
Application Fields of ER4047 Aluminum Welding Wire
Automotive Industry
Radiators and cooling systems using automotive aluminum microchannel tubes
Heat exchangers made with brazed aluminum sheet
Transmission oil cooler and EGR cooler repair
HVAC / Refrigeration Equipment
Heat exchanger assemblies made with aluminum brazing sheet where furnace brazing is specified
Microchannel condensers & evaporators
Tube-fin refrigeration assemblies using suitable aluminum brazing strip and other heat exchanger components
Aerospace Structures
Automatic pulse MIG welding of fuselage skins and wing panels
Seam welding of internal and external fuel tanks and pressurization tanks
Defect repair of 7005 and 6061 machined frame beams
Die Casting Repair and Maintenance
Automatic pulse MIG welding for fuselage skins & wing panels
Seam welding for fuel & pressurization tanks
Repair of 7005/6061 machined frame beams
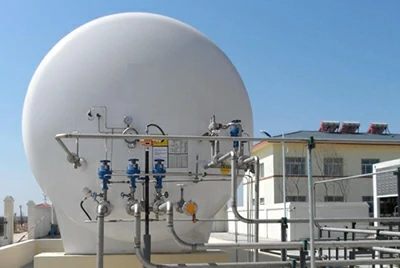
Sealed and Pressurized Aluminum Containers
Circumferential welding of LH₂ and LN₂ tanks
High-pressure A/C receivers
Aerospace pneumatic/hydraulic fittings
High-Temperature Heat Exchange Equipment
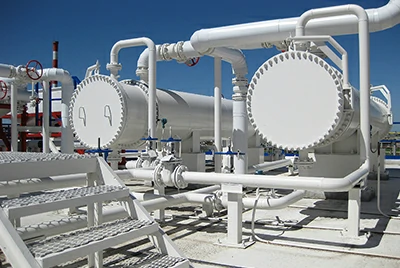
Microchannel welding for solar collector panels
Aluminum heat exchangers for industrial furnaces
Mid/high-temp radiators for generator sets
Why Choose Chalco?
Chalco supplies ER4047 aluminum welding wire as part of its broader aluminum welding and brazing materials range, supporting industrial customers with welding filler products, brazing materials, alloy specifications, and export packaging requirements.
- Globally Certified Quality Production Lines: The factory is certified by ISO 9001 and IATF 16949 dual quality management systems, with an annual production capacity of 8,000 tons and full batch traceability.
- Ultra-High Precision and Moisture Protection: Wire drawing tolerance is strictly controlled within ±0.02 mm. Before leaving the factory, it undergoes vacuum drying and degassing, and is then packaged in aluminum foil composite bags to ensure long-term storage without moisture absorption.
- Ultra-Fast Delivery Capability: Common wire diameters ranging from Ø 0.8–4.0 mm are in stock, with a minimum order quantity starting from S100 (0.5 kg). All in-stock items are shipped to your door within 72 hours.
- One-Stop Technical Support: Enjoy 24-hour response from engineers upon placing an order, providing exclusive welding parameter guidance, base material comparison test plates, and COA/COC reports, truly achieving "online ordering, offline worry-free."
Click the "Get a Sample" button on the right to let our professional team quickly customize an ER4047 welding solution for you.
Instant Quote
Technical Reference for ER4047 Aluminum Welding Wire
Chemical Composition of ER4047 Aluminum Welding Wire
| Elements | Value% |
| Si | 11.0 – 13.0 |
| Fe | ≤0.80 |
| Cu | ≤0.30 |
| Zn | ≤0.20 |
| Mn | ≤0.10 |
| Others-Each | ≤0.05 |
| Others-Total | ≤0.15 |
| Al | Rem |
ER4047 aluminum alloy's primary alloying element is silicon, with trace amounts of iron, copper, zinc, manganese, and magnesium. This composition provides it with stable performance in oxidizing and high-temperature environments.
Welding Positions for ER4047 Aluminum Welding Wire
ER4047 supports all-position welding (except for specialized vertical-down in-furnace welding). The six common posture diagrams are shown below:
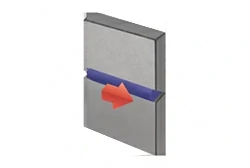
2G Horizontal Welding
Weld axis is horizontal in a vertical plane, ensuring stable pool and easy penetration. Ideal for side joints on medium plates or continuous pipe-to-plate welding.
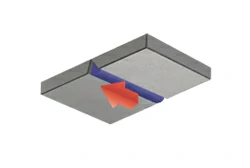
4G Overhead Welding
Welds beneath the workpiece, needing precise droplet control to avoid sagging. Used for floor panels, ceilings, and reverse structural welding.
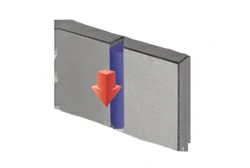
3G Vertical Down Welding
Torch moves downward along the joint for fast welding. Best for thin sheets to increase speed, but demands precise control to avoid droplet sag.
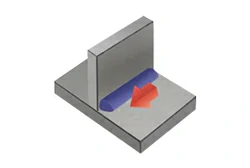
2F Horizontal Fillet Welding
Welds corner joints between horizontal and vertical plates, filling angles with smooth beads for strength and appearance—common in frames and structures.
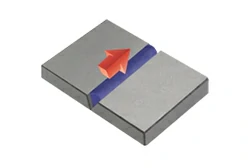
1G Flat Welding
Weld lies on a horizontal plane. Offers optimal penetration and bead width for long, straight seam welding and large-area fabrication.
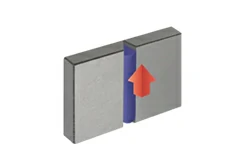
3F Vertical Up Fillet Welding
Fills vertical corner joint bottom-up, ensuring uniform penetration and tie-in—ideal for reliable fillet welds on load-bearing parts.
Typical Mechanical Properties of ER4047 GTAW Butt Joint Welds
| BASE ALLOY | AS WELDED | POST WELD HEAT TREAT AND AGE | |||||||
| BASE ALLOY | UTS (KSI) | UYS (KSI) | ELONG (%) | UTS (KSI) | UYS (KSI) | ELONG (%) | UTS (KSI) | UYS (KSI) | ELONG (%) |
| 2014-T6 | 70 | 60 | 13 | 34 | 28 | 4 | 50 | -- | 2 |
| 6061-T4 | 35 | 21 | 22 | 27 | 18 | 8 | 352 | -- | 82 |
| 6061-T6 | 45 | 40 | 12 | 27 | 18 | 8 | 44 | 40 | 5 |
| 6063-T4 | 25 | 22 | 22 | 20 | 10 | 12 | 30 | -- | 13 |
ER4047 Aluminum Welding Wire MIG Reference Process Parameters
When using ER4047 aluminum, precise control of welding parameters is crucial for achieving high-quality joints and minimizing defects. Its high silicon content (11-13%), excellent fluidity, and low shrinkage make it ideal for various welding applications. Below are specific parameters:
| Wire diameter | Welding posture | Current (A) | Voltage (V) | Wire feed speed in/min (m/min) | Deposition rate lbs/hr (kg/hr) | CTWD in (mm) |
| 0.035" (0.9 mm) | All Position | 135 | 20.7 | 400 (10.2) | 6.4 (2.9) | ½ (13) |
| 0.035" (0.9 mm) | All Position | 145 | 21.3 | 450 (11.4) | 7.2 (3.3) | ½ (13) |
| 0.035" (0.9 mm) | All Position | 160 | 21.8 | 500 (12.7) | 8.0 (3.6) | ½ (13) |
| 0.035" (0.9 mm) | All Position | 165 | 22 | 550 (14.0) | 8.8 (4.0) | ½ (13) |
| 0.035" (0.9 mm) | All Position | 185 | 22.3 | 600 (15.2) | 9.6 (4.3) | ½ (13) |
| 3/64" (1.2 mm) | All Position | 180 | 21.4 | 300 (7.6) | 7.9 (3.6) | ½ (13) |
| 3/64" (1.2 mm) | All Position | 210 | 21.8 | 350 (8.9) | 9.2 (4.2) | ½ (13) |
| 3/64" (1.2 mm) | All Position | 225 | 22.4 | 400 (10.2) | 10.5 (4.8) | ½ (13) |
| 3/64" (1.2 mm) | All Position | 260 | 24 | 450 (11.4) | 11.9 (5.4) | ⅝ (16) |
| 3/64" (1.2 mm) | All Position | 270 | 24.3 | 500 (12.7) | 13.2 (6.0) | ⅝ (16) |
ER4047 vs ER4043 vs 4943 – Selection Comparison of Aluminum-Silicon Filler Wires
| Comparison items | ER4047(Al-Si 12) | ERER4043(Al-Si 5) | ER4943(Al-Si 6.5-Mg 0.6) |
| Main alloying elements (wt %) | Si 11 – 13 | Si 4.5 – 6.0 | Si 6.3 – 7.0, Mg 0.45 – 0.9 |
| Solidus / liquidus ≈ °C | 532 / 571 | 566 / 582 | 565 / 574 |
| Pot fluidity | ★★★★☆ (highest) | ★★★☆ | ★★★☆ |
| Hot cracking tendency (weld 6xxx) | ★☆☆☆ (lowest) | ★★☆☆ | ★★☆☆ |
| Weld shrinkage | Minimum | Medium | Medium |
| Anodized color | Dark grey-black, maximum color difference | Light grey, easier to match the parent material | Between the two, with minimal color difference |
| Typical tensile strength (6061-T6 base metal, single pass / PWHT) | ~ 140 MPa/ 210 MPa | ~ 150 MP/ 220 MPa | ~ 170 MP/ 260 MPa |
| Shear strength (fillet weld) | Highest | High | High |
| Can be re-aged with 6xxx | No | No | Can be aged (Mg + Si) |
| Thermal / electrical conductivity | ★★★☆ | ★★★☆ | ★★☆☆ |
| Advantages | Lowest melting point | Most versatile | Significant improvement in post-weld strength |
| Typical applications | Excellent fluidity | Price friendly | Replaces 5356/ER4043 to reduce weight |
| Compatible with base metal | Preferred for brazing, hermetic sealing | Small color difference of decorative parts | High-strength welding of 6xxx structural parts |
- If you require airtight brazing, thin-walled heat exchangers, or crack-sensitive castings, choose ER4047.
- If you require general structural/decorative welding, cost sensitivity, and minimal color difference, consider ER4043.
- If you require high-strength 6xxx series or structural components needing PWHT for strength recovery, ER4047 can be an option for the root pass with a cap of ER4943 or ER5356.
Still hesitating? Tell me the base material grade, thickness, and target strength, and Chalco engineers will provide exclusive filler wire recommendations and welding parameter guidance within 24 hours.
Instant QuoteRelated Aluminum Brazing Materials

FAQ
How to choose between ER4047 and ER4043?
If your main applications involve 6xxx thin plates, heat exchanger furnace brazing, or casting crack repair, requiring high fluidity and low cracking rate – ER4047 is your first choice. If it's mainly general structural or decorative welding and you are sensitive to the color difference after anodizing, you can continue to use the lower-cost and lighter-colored ER4043. If you are still unsure, tell us the base material grade and thickness, and our engineers will provide a recommendation within 24 hours.
The ER4047 weld will turn dark gray after anodizing. Can this be solved?
The high silicon content of ER4047 determines its dark gray undertone after anodizing. There are three common solutions:
- Backside or corner welding – the weld is not on the visible surface.
- Overall re-spraying or powder coating after anodizing.
- Multi-pass process: use ER4047 for the root pass and overlay with 5356/4943 to match the base material color.
Chalco can provide color matching test plates and dual filler wire process guidance for your verification.
What is the minimum purchase quantity? Can I get a sample first?
Commonly stocked Ø 0.8–4.0 mm welding wires all support sampling of 1 S100 spool (0.5 kg) or 1 kg TIG straight rods; stock items can be shipped within 72 hours. Large volume orders can be customized with 150 kg large spools or 1 m TIG straight rods as needed.
Can ER4047 weld high-magnesium 5xxx or high-zinc 7xxx series alloys?
Not recommended. 5xxx series alloys with Mg >3% (such as 5083, 5456) and high-Zn 7xxx series alloys (such as 7075) are highly sensitive to hot cracking with Si-based welding wires. It is recommended to use ER5356/ER5556 or dedicated Zn-Mg based filler wires. If it is necessary to use ER4047, the risk can be reduced by preheating and using a dual-pass process. Please consult our technical team for details.
Is post-weld heat treatment necessary? Can the strength be recovered?
ER4047 is a non-heat-treatable strengthening alloy, so it can be put into use after welding without solution treatment and aging. For base materials such as 6061-T6, the joint strength is approximately 60-70% of the base material. If further strength improvement is needed, ER4047 can be used for the root pass of fillet welds to ensure airtightness, followed by an overlay of 4943 and short-term artificial aging.
How should ER4047 welding wire be stored? How long should it be used up after opening?
The welding wire is vacuum-dried and packaged before leaving the factory. It can be stored for 12 months in a storage environment with <60% RH and 15-25 °C. It is recommended to use it up within 30 days after opening. If the machine is stopped midway, it can be vacuum-sealed again or stored in a sealed container with 2 × silica gel desiccant packs to avoid moisture absorption leading to porosity.
Chalco can provide you the most comprehensive inventory of aluminum products and can also supply you customized products. Precise quotation will be provided within 24 hours.
Get a quote