Chalco supplies aluminum welding wire and filler metals in ER4043, ER5356, ER5183, ER4943, ER4643, and other aluminum alloy grades. Our range supports MIG/GMAW welding and suitable TIG/GTAW filler applications, helping manufacturers select materials according to base alloy compatibility, required weld properties, and welding processes.
For industrial and OEM procurement, Chalco supports welding wire specification review, diameter and packaging selection, material documentation, and supply planning. Our broader aluminum welding and brazing materials range also covers filler rods, welding electrodes, and other joining consumables for different manufacturing requirements. Customers can compare filler grades, technical reference data, and available supply options below, or submit their specifications for a quotation.
Aluminum Welding Wire Grades, Sizes and Supply Options
Alloy series: 4043, 5356, 5556, 5183, 4643, 4943, 4047, 5554, 1100 Click to [alloy detail]
Welding Methods: Aluminum MIG welding wire is used as a continuously fed electrode in GMAW, while TIG/GTAW typically uses separate filler rods, including ER5356 aluminum TIG filler rods, or compatible automatic filler-feeding systems.
Welding Positions: flat, horizontal, vertical (up/down), overhead
Surface Requirements: Clean wire surfaces and suitable winding conditions according to the welding process and agreed product specifications.
Common Diameters: 0.030" (0.8mm), 0.035" (0.9mm), 0.045" (1.2mm), 1/16" (1.6mm), 3/64" (1.2mm), 5/64" (2.0mm), etc.
Wire Condition/Tolerance: F temper; ISO 544 h9 ±0.02mm
Packaging: 0.5kg, 1kg, 5kg, 15kg spools; 300mm/400mm cores; custom large spools (50-250kg) and packaging tailored to MIG torch systems
Aluminum Welding Wire Grades and Base Metal Compatibility
Aluminum welding wire selection involves different Al-Si and Al-Mg filler grades, each with its own base alloy compatibility and welding characteristics. The 16 aluminum welding wire grades overview covers a broader range of filler classifications, while the commonly requested grades below are presented with their composition, applications, and welding considerations.
Top choice for welding: 4043 and 5356 —— Best-selling aluminum welding wires
-
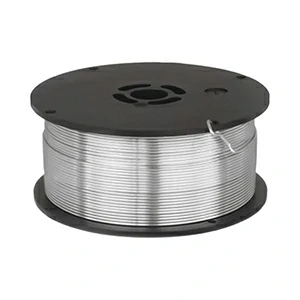
Compatible base alloys: 6xxx series aluminum (e.g., 6061, 6063)
Welding system: GMAW/MIG (manual, automatic, robotic); shielding gas: pure argon or Ar-He mix
-
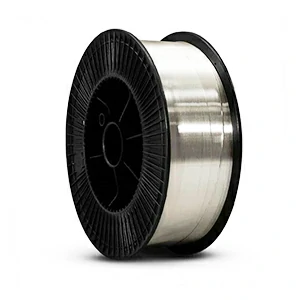
Compatible base alloys: 5xxx series (e.g., 5052, 5083, 5454, 5356), also suitable for 6xxx series
Welding system: GMAW/MIG (manual, automatic); shielding gas: pure argon
| Alloy | Si (%) | Fe (%) | Cu (%) | Mn (%) | Mg (%) | Cr (%) | Zn (%) |
| 4043 | 4.5–6.0 | ≤0.80 | ≤0.30 | ≤0.05 | ≤0.05 | — | ≤0.10 |
| 5356 | ≤0.25 | ≤0.40 | ≤0.10 | 0.05–0.20 | 4.5–5.5 | 0.05–0.20 | ≤0.10 |
- Lower melting point, good weld pool flow
- Strong resistance to hot cracking
- Less spatter, smooth and neat weld bead
- Weld bead can be anodized gray or dark gray
- High weld strength and load capacity
- Excellent corrosion resistance, ideal for marine environments
- Good weld metal ductility, better crack resistance than standard Al-Mg wires
- Weld bead color close to base metal, good for decorative use
4643 Aluminum Welding Wire for Heat-Treatable Aluminum Alloys
-
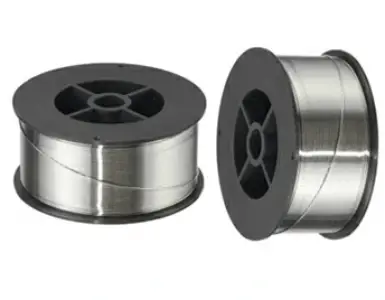
4643 aluminum welding wire is an Al-Si-Mg filler metal for selected heat-treatable aluminum alloy joints, with attention to welding procedures and post-weld properties.
Compatible base alloys: Selected 6xxx alloys, including 6061 and 6063, subject to filler selection and welding procedures.
Welding systems: Conventional and robotic MIG wire feeding systems
| Element | Si | Fe | Cu | Mn | Mg | Zn | Ti | Be |
| Range % | 3.6–4.6 | ≤0.80 | ≤0.10 | ≤0.05 | 0.10–0.30 | ≤0.10 | ≤0.15 | ≤0.0008 |
4943 aluminum welding wire – upgraded 4043 for higher strength welding
-
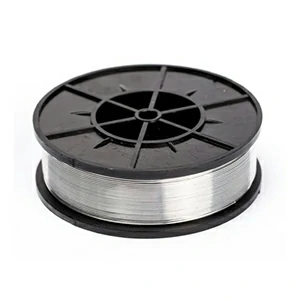
4943 aluminum welding wire is an Al-Si-Mg filler metal with higher typical as-welded strength than ER4043 under comparable test conditions.
Compatible base alloys: 6xxx series heat-treated aluminum alloys (e.g., 6061-T6)
Welding systems: Standard/automatic MIG systems; pure argon recommended
| Element | Si | Fe | Cu | Mn | Mg | Others | Al (balance) |
| Range % | ~5.5 | ≤0.80 | ≤0.10 | ≤0.15 | — | — | Remainder |
5183 aluminum welding wire – marine-grade high strength and corrosion resistance
-
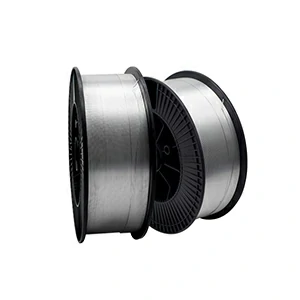
5183 aluminum welding wire is a high-magnesium alloy offering high weld strength and seawater corrosion resistance for marine and structural applications.
Compatible base alloys: High-strength 5xxx series (e.g., 5083, 5456, 5056)
Welding systems: MIG welding (manual, automatic); shielding gas: pure argon
| Element | Si | Fe | Cu | Mn | Mg | Cr | Zn | Ti |
| Range % | ≤0.40 | ≤0.40 | ≤0.10 | 0.50–1.00 | 4.3–5.2 | 0.05–0.25 | ≤0.25 | ≤0.15 |
5556 aluminum welding wire – military-grade strength and fatigue resistance
-
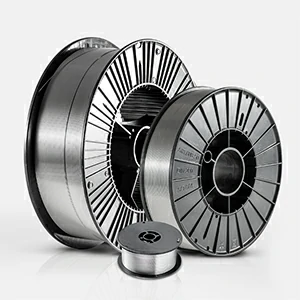
5556 aluminum welding wire is a high-strength Al-Mg alloy with fatigue resistance and stability for demanding structural welding.
Compatible base alloys: High-strength 5xxx series (e.g., 5086, 5456, 5083)
Welding systems: Standard, automated, and high-load MIG systems
| Element | Si | Fe | Cu | Mn | Mg | Cr | Zn | Ti |
| Range % | ≤0.25 | ≤0.40 | ≤0.10 | 0.50–1.0 | 4.7–5.5 | 0.05–0.20 | ≤0.25 | ≤0.20 |
4047 aluminum welding wire – high-silicon wire for superior sealing and flow
-
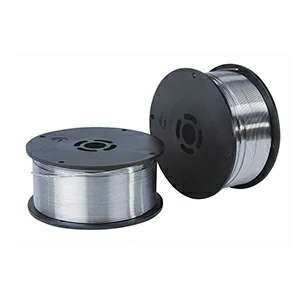
4047 aluminum welding wire is a high-silicon aluminum alloy with excellent flow and airtight welds, ideal for casting repair and precision sealing applications.
Compatible base alloys: Aluminum castings (e.g., A356), specialty alloys, heat exchanger substrates
Welding systems: MIG automatic feed and precision equipment; pure argon shielding gas recommended
| Element | Si | Fe | Cu | Mn | Mg | Zn | Al (balance) |
| Range % | 11–13 | ≤0.80 | ≤0.30 | ≤0.15 | ≤0.10 | ≤0.20 | Remainder |
5087 Aluminum Welding Wire – Zirconium-enhanced alloy for superior corrosion resistance and flexibility
-
5087 aluminum welding wire contains ~4.5% magnesium and zirconium for grain refinement, offering high strength, corrosion resistance, bendability, and reduced hot cracking sensitivity.
Compatible base alloys: Selected 5xxx, 6xxx, 7xxx alloys, including 5083, 6082, 7005, 7020
Applications: Shipbuilding, storage tanks, high-speed trains, automotive
| Element | Si | Fe | Cu | Mn | Mg | Cr | Zn | Ti |
| Range % | ≤0.25 | ≤0.40 | ≤0.05 | 0.70–1.10 | 4.5–5.2 | 0.05–0.25 | ≤0.25 | ≤0.15 |
5754 Aluminum Welding Wire – high-magnesium alloy with excellent strength and corrosion resistance
-
5754 aluminum welding wire contains about 3% magnesium, offering moderate strength and good corrosion resistance.
Compatible base alloys: 3% magnesium cast/wrought alloys, 5xxx wrought alloys, and some 6xxx alloys
Applications: Structural and corrosion-resistant aluminum welding
| Element | Si | Fe | Cu | Mn | Mg | Cr | Zn | Ti |
| Range % | ≤0.40 | ≤0.40 | ≤0.10 | ≤0.50 | 2.6–3.6 | ≤0.30 | ≤0.20 | ≤0.15 |
More optional aluminum alloy and welding wire alloy customization services
In addition to standard aluminum welding wire grades, Chalco can review selected specialty filler metal requirements according to material, composition, welding process, and order specifications. Availability of non-standard alloys and other material categories should be confirmed separately.
-
1100 al welding wire
1100 is a pure aluminum welding wire for 1050, 1060, and 1070 alloys, offering good ductility and conductivity—ideal for low-strength joints, electrical parts, and decorative welds.
-
6061 al welding wire
Though mainly used as base material, 6061 is also available as welding wire for specific self-welding or custom jobs requiring precise composition match with the base metal.
-
5554 al welding wire
A medium-strength aluminum-magnesium wire for welding 5454 and 5554 alloys, commonly used in fuel tanks, marine parts, and other corrosion-resistant applications.
-
Aluminum bronze welding wire
Offers excellent corrosion resistance and strength; used for repairing copper alloy parts like pumps and valves, and for copper-aluminum transition joints.
-
Copper alloy welding wire
Suitable for welding copper, copper alloys, and copper-stainless steel; known for great conductivity in electrical, thermal, and precision applications.
-
Nickel-aluminum welding wire
Resistant to high temperatures and corrosion; ideal for surfacing and structural repairs in power plants, nuclear facilities, and wear-prone alloy parts.
-
Titanium welding wire
Excellent strength-to-weight ratio, corrosion resistance, and high-temperature performance; suitable for aerospace, chemical processing, and marine applications.
-
Al-Mg-Sc welding wire
Enhanced strength, toughness, and weldability through rare earth element modification; ideal for demanding structural and automotive applications.
-
Wire+arc additive manufacturing wire
High purity and consistent feed characteristics ensure reliable performance in additive manufacturing; suitable for prototyping and lightweight structural components.
For a quotation, please share your required welding wire grade, diameter, packaging, quantity, and application. Chalco can help confirm suitable product options and supply details based on your specifications.
Aluminum Welding Wire Selection by Base Alloy
| Base metal | 7003 | 6061 6063 6101 | 5086 5083 5056 | 5154 5454 | 5052 | 5005 | 2219 | 2014 2017 | 3004 | 1200 | 1100 3003 | 1070 1050 |
| 1070 1050 |
5356 (2)(4)(5) |
4043 (5)(7) |
5356 (2) |
5356 (2)(4)(5) |
4043 (2)(5) |
1100 (1)(4)(5) | 4145 (4)(5) | 4145 | 4043 (2)(5) | 1200 (1)(4)(5) | 1100 (1)(4)(5) | 1070 (1)(4)(5) |
| 1100 3003 | 5356 (2)(4)(5) | 4043 (5)(7) | 5356 (2) | 5356 (2)(4)(5) | 4043 (2)(5) | 1100 (1)(4)(5) | 4145 (4)(5) | 4145 | 4043 (2)(5) | 1200 (1)(4)(5) | 1100 (1)(4)(5) | |
| 1200 |
5356 (2)(4)(5) |
4043 (5)(7) |
5356 (2) |
5356 (2)(4)(5) |
4043 (2)(5) |
1100 (1)(4)(5) |
4145 (4)(5) |
4145 |
1200 (1)(4) |
1200 (1)(4)(5) |
||
| 3004 |
5356 (2)(4) |
4043 (2) (3) (5)(7) |
5356 (2) |
5356 (2)(3)(4)(5) |
4043 (2)(3)(4)(5) |
5356 (2)(3)(4) |
4145 (4)(5) |
4145 |
5356 (2)(3)(4) |
1200 (1)(4)(5) |
||
| 2014 2017 | 4145 | 4145 |
4145 (8) |
4145 (8) |
||||||||
| 2219 |
4043 (5) |
4043 (5)(6) |
4043 (5) |
4043 (5) |
4043 (5)(6) |
2319 (4)(5)(6) |
||||||
| 5005 |
5356 (2)(3) |
4043 (2) (3) (5)(7) |
5356 (2) |
5356 (2)(3) |
5356 (2)(3)(4)(5) |
5356 (2)(3)(4)(5) |
||||||
| 5052 |
5356 (2)(3) |
4043 (2) (3) (5)(7) |
5356 (2) |
5356 (2)(3) |
5356 (2)(3)(4) |
|||||||
| 5154 |
5356 (2)(3) |
5356 (2)(3)(4) |
5356 (2)(3) |
5356 (2)(3) |
Remark:; (1) can adopt 1100 or 1200 (2) can adopt 5356.5556 or 5183; (3) can adopt 5654 or5554; (4) according to usage can adopt4043; (5) can adopt 4047; (6) can adopt 4145; (7) adopt 5356 when apears chromatic abberation after anodic process; (8) can adopt 2319 |
|||||||
| 5086 5083 |
5356 (2) |
5356 (2) |
5356 (2) |
|||||||||
| 6061 6063 |
5356 (2)(3) (4)(5) |
4043 (2) (3) (5) |
||||||||||
| 7003 |
5356 (2) |
|||||||||||
Aluminum Welding Wire Technical Data and Standards
| Chalco aluminum welding wire products weld mechanical properties (reference value) | |||
| Alloy | Tensile strength (MPa) | Yield strength (MPa) | Elongation (%) |
| 4043 Weld | 170–190 | 90–110 | 6–10 |
| 5356 Weld | 250–280 | 110–130 | 11–18 |
| 4943 Weld | 230–260 | 130–150 | 10–14 |
| 5183 Weld | 270–300 | 130–160 | 10–16 |
| 5556 Weld | 280–310 | 150–180 | 8–12 |
| The weld performance varies with the thickness of the base material, welding process and heat treatment status. The above are reference values for standard test plate tests. | |||
| Aluminum Welding Wire Key Process Parameters Reference Table | |||||||
| Welding Wire Model | Typical Diameter (mm) | Recommended Current Range (A) | Recommended Voltage Range (V) | Wire Feed Speed (m/min) | Shielding Gas | Welding Method | Main Application Areas |
| ER4043 (Al-Si) | 0.8 / 1.0 / 1.2 | 90 - 180 | 18 - 22 | 4.5 - 9.0 | 100% Ar | MIG / TIG | Thin aluminum sheets, automotive, electronics |
| ER5356 (Al-Mg) | 0.8 / 1.0 / 1.2 | 100 - 200 | 19 - 23 | 5.0 - 9.5 | 100% Ar or Ar+He mix | MIG / TIG | Marine equipment, corrosion-resistant structures |
| ER5183 (Al-Mg) | 1.0 / 1.2 / 1.6 | 150 - 280 | 20 - 24 | 6.5 - 12.0 | 100% Ar or Ar+He mix | MIG / TIG | Shipbuilding, high-strength structures |
| ER5556 (Al-Mg) | 1.0 / 1.2 | 120 - 220 | 19 - 23 | 5.5 - 10.0 | 100% Ar | MIG / TIG | Thick plate welding, pressure vessels |
| ER1100 (Al-99.0%) | 0.8 / 1.0 | 70 - 140 | 17 - 21 | 3.5 - 7.5 | 100% Ar | MIG / TIG | General purpose aluminum welding |
| Shielding Gas and Arc Transfer Modes Table | ||
| Shielding Gas Type | Arc Transfer Mode | Description |
| 100% Ar | Pulsed Spray Transfer | Good weld appearance, suitable for thin plate welding |
| Ar + 25% He | Spray Transfer | High heat input, suitable for thick plate and high-strength welding |
| Ar + 5-10% CO₂ | Globular Transfer | Stable droplet transfer, high welding efficiency, wide applicability |
| Packaging Specifications and Certifications Table | |
| Packaging Specifications | Various options: 5 kg / 15 kg / 20 kg, etc. |
| Product Standards | AWS A5.10 — American standard for aluminum alloy welding wire (ER series grades) |
| ISO 18273 — International standard for aluminum welding filler materials (AlSi, AlMg naming) | |
| GB/T 10858 — Chinese standard for aluminum and aluminum alloy welding wire | |
| Documentation Support | COA, MSDS, ROHS, REACH, CE and other document support |
| Customization Capability | Alloy composition adjustment and packaging customization available |
| Chalco aluminum welding wire products implementation standards | |
| AWS A5.10 | American standard aluminum alloy welding wire standard (ER series grade) |
| ISO 18273 | International aluminum welding filler material standards (naming methods such as AlSi, AlMg, etc.) |
| GB/T 10858 | China Aluminum and Aluminum Alloy Welding Wire Standards |
| Can provide: COA, MSDS, ROHS, REACH, CE and other document support. | |
Chalco supports aluminum welding wire specification review and supply planning based on your technical requirements. Share your required alloy grade, wire diameter, applicable standards, packaging, and order quantity to confirm available options, documentation, and quotation details.
MIG/TIG Welding Methods and Equipment Compatibility
Aluminum filler metal selection should account for the welding process, equipment configuration, wire feeding method, and qualified welding procedure. MIG/GMAW commonly uses continuously fed electrode wire, while TIG/GTAW typically uses a separate filler rod or a compatible automatic filler-feeding system. Equipment suitability and welding parameters should be confirmed for each application.
- MIG/GMAW: Continuously fed aluminum electrode wire for suitable manual, mechanized, and robotic welding applications.
- TIG/GTAW: Filler rods or compatible automatic filler-feeding systems selected according to the welding procedure.
- Pulsed MIG: Welding parameters and filler wire selection should match the equipment, material thickness, and required weld characteristics.
- Automated Welding: Wire feeding stability, spool configuration, surface condition, and batch consistency are important for repeatable production.
| Welding method | Recommended welding wire type | Alloy Recommendation | Applicable instructions |
| MIG welding | Aluminum solid wire (MIG Solid Wire) | 4043, 5356, 4943 | Mainstream configuration for conventional industrial applications, suitable for welding 6 series and 5 series aluminum alloys |
| Automated MIG welding | High-precision solid welding wire (Robotic Grade Wire) | 4043, 4943, 5183 | It has higher requirements on welding wire consistency and is suitable for batch welding and welding robots. |
| Flux core MIG welding | Flux-Cored Aluminum Wire | Special composite alloys (such as customized 4045 base) | A small amount of welding is used in a gas-free environment or in special locations. It is not a mainstream product. |
| TIG automatic wire feeding system | Precision controlled wire feeding aluminum welding wire (for TIG automatic system) | 4043,5356 | Suitable for automatic TIG process, coiled aluminum wire can be used when there is a special control system |
| SMAW manual welding | Non-wire products → Use aluminum welding rod/Stick Electrode | E4043, E5356, etc. |
| Typical operating parameters (for groovewelding) | |||||||
| Base Metal Thickness (mm) | Welding Position | Weld Spacing (mm) | Welding Pass | Wire Diameter (mm) | Current (A) | Voltage (V) | Argon Flow (cfh) |
| 1.6 | F | None | 1 | 0.8 | 70-110 | 15-20 | 25 |
| 1.6 | F | 2.4 | 1 | 0.8 | 70-110 | 15-20 | 25 |
| 2.4 | F, V, H, O | None | 1 | 0.8-1.2 | 90-150 | 18-22 | 30 |
| 2.4 | F, V, H, O | 3.2 | 1 | 0.8-1.2 | 110-130 | 18-22 | 30 |
| 3.2 | F, V, H | 0-2.4 | 1 | 0.8-1.2 | 120-150 | 20-24 | 30 |
| 3.2 | F, V, H, O | 3-16 | 1 | 0.8-1.2 | 110-135 | 19-23 | 30 |
| 5 | F, V, H | 0-1.6 | 1F, 1R | 0.8-1.2 | 130-175 | 22-26 | 35 |
| 5 | F, V, H | 0-1.6 | 1 | 1.2 | 140-180 | 23-27 | 35 |
| 5 | O | 0-1.6 | 2F | 1.2 | 170-175 | 23-27 | 60 |
| 5 | F, V | 2.4-5 | 2 | 1.2-1.6 | 140-185 | 23-27 | 35 |
| 5 | H, O | 5 | 3 | 1.2 | 130-175 | 23-27 | 60 |
| 6.5 | F | 0-2.4 | 1F, 1R | 1.2-1.6 | 175-200 | 24-28 | 40 |
| 6.5 | F | 0-2.4 | 2 | 1.2-1.6 | 185-225 | 24-29 | 40 |
| 6.5 | V, H | 0-2.4 | 3F, 1R | 1.2 | 165-190 | 25-29 | 45 |
| 6.5 | O | 0-2.4 | 3F, 1R | 1.2 | 180-200 | 25-29 | 70 |
| 6.5 | F, V | 3.2-6.5 | 2-3 | 1.2-1.6 | 175-225 | 25-29 | 60 |
| 6.5 | O, H | 1-4 | 4-6 | 1.2-1.6 | 170-200 | 25-29 | 60 |
| 10 | F | 0-2.4 | 1F, 1R | 1.6 | 225-290 | 26-29 | 50 |
| 10 | F | 0-2.4 | 2F, 1R | 1.6 | 210-275 | 26-29 | 50 |
| 10 | V, H | 0-2.4 | 3F, 1R | 1.6 | 190-220 | 26-29 | 55 |
| 10 | O | 0-2.4 | 6F, 1R | 1.6 | 200-250 | 26-29 | 80 |
| 10 | F, V | 6.5-10 | 1 | 1.6 | 210-290 | 26-29 | 50 |
| 10 | O, H | 10 | 8-10 | 1.6 | 190-260 | 26-29 | 80 |
| 20 | V, H, O | 0-1.6 | 8F, 1R | 1.6 | 240-300 | 26-30 | 80 |
| 20 | F | 0-1.6 | 3F, 1R | 1.6 | 270-330 | 26-30 | 80 |
| 20 | V, H, O | 0-1.6 | 6F, 0R | 1.6 | 230-280 | 26-30 | 80 |
|
F = Flat Position V = Vertical Position H = Horizontal Position O = Overhead Position For 5XXX series welding wires, select the highest and lowest current and voltage specified; For 1XXX and 4XXX series welding wires, select the lower current and higher voltage. |
|||||||
| Typical operating parameters (for fillet welding and lap welding) | |||||||
| Base Metal Thickness (mm) | Welding Position (1) | Weld Pass | Electrode Diameter (mm) | Direct Current (2) (A) | Arc Voltage (2) (V) | Argon Flow Rate (cfh) | Welding Speed (ipm/pass) |
| 2.4 | F, V, H, O | 1 | 0.8 | 100-130 | 18-22 | 30 | 24-30 |
| 3.2 | F | 1 | 0.8-1.2 | 125-150 | 20-24 | 30 | 24-30 |
| 3.2 | V, H | 1 | 0.8 | 110-130 | 19-23 | 30 | 24-30 |
| 3.2 | O | 1 | 0.8-1.2 | 115-140 | 20-24 | 40 | 24-30 |
| 5 | F | 1 | 1.2 | 180-210 | 22-26 | 30 | 24-30 |
| 5 | V, H | 1 | 0.8-1.2 | 130-175 | 21-25 | 35 | 24-30 |
| 5 | O | 1 | 0.8-1.2 | 130-190 | 22-28 | 45 | 24-30 |
| 6.5 | F | 1 | 1.2-1.6 | 170-240 | 24-28 | 40 | 24-30 |
| 6.5 | V, H | 1 | 1.2 | 170-210 | 23-27 | 45 | 24-30 |
| 6.5 | O | 1 | 1.2-1.6 | 190-220 | 24-28 | 60 | 25-30 |
| 10 | F | 1 | 1.6 | 240-300 | 26-29 | 50 | 18-25 |
| 10 | V, H | 3 | 1.6 | 190-240 | 24-27 | 50 | 24-30 |
| 10 | O | 3 | 1.6 | 200-240 | 25-28 | 85 | 24-30 |
| 20 | H, V | 4-6 | 1.6 | 260-310 | 25-20 | 70 | 24-30 |
| 20 | O | 10 | 1.6 | 275-310 | 25-29 | 85 | 24-30 |
|
F = Flat Position V = Vertical Position H = Horizontal Position O = Overhead Position For 5XXX series welding wires, select the highest and lowest current and voltage specified; For 1XXX and 4XXX series welding wires, select the lower current and higher voltage. |
|||||||
Chalco can assist with aluminum filler metal selection based on your base alloy, welding method, equipment configuration, and production requirements. Share your welding specifications to discuss suitable wire grades, available supply options, and technical documentation.
Aluminum Welding Wire Applications and Industry Supply
Chalco supports aluminum welding wire requirements across transportation, marine fabrication, industrial structures, and equipment manufacturing. Filler metal selection, wire specifications, and documentation can be reviewed according to the customer's base alloy, welding process, and production requirements.
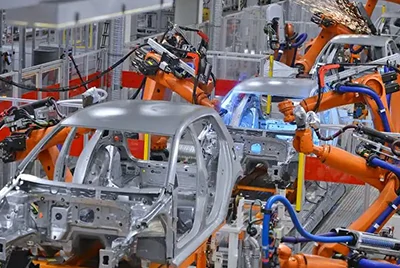
Automotive Manufacturing: Aluminum welding consumables can be selected for compatible vehicle frames, fabricated components, and automated production lines. Related assemblies such as automotive welded aluminum tubes involve base alloy and joining-process requirements that must be considered when evaluating filler materials.
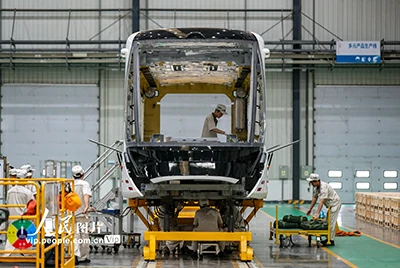
Rail Transit: Filler metal and wire diameter coordination for qualified aluminum vehicle structures and related fabrication requirements.
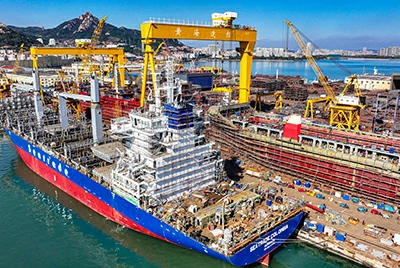
Shipbuilding and Offshore Equipment: ER5183, ER5356, and other suitable filler alloys may be considered when welding compatible marine aluminum structures, including those fabricated from 5083 marine aluminum plate. Final filler selection depends on the base alloy, service environment, and approved welding requirements.
Building and Industrial Structures: Welding material requirements for suitable aluminum frames, railings, equipment housings, and fabricated assemblies.
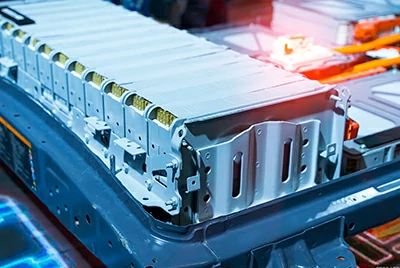
New Energy and Transportation Equipment: Support for selected aluminum battery enclosures, trays, and related welded structures subject to approved material and joining requirements.
General Industrial Fabrication: Welding wire grades, supply forms, and order documentation can be coordinated for industrial equipment and repeat manufacturing needs.
Why Choose Chalco as Your Aluminum Welding Wire Supplier?
- Alloy Selection: ER4043, ER5356, ER5183, ER4943, and other filler grades for different aluminum base alloys, welding processes, and joint performance requirements.
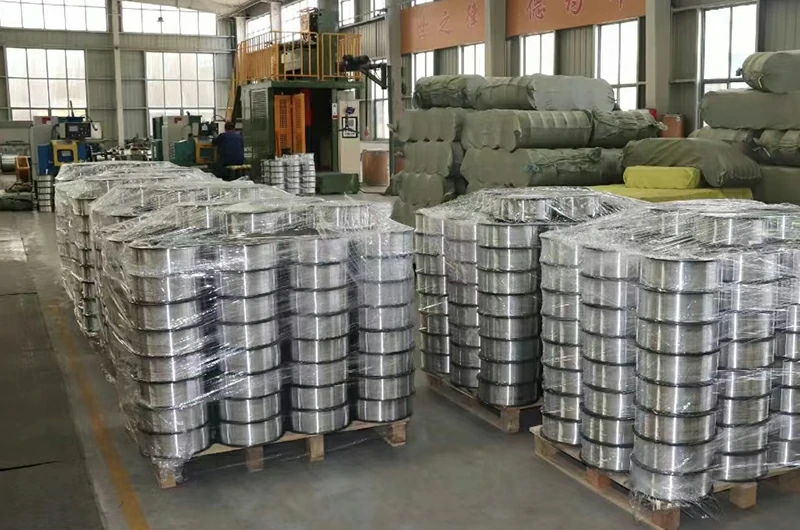
- Consistent Wire Feeding: Wire diameter, surface condition, and winding quality are controlled according to agreed specifications to support stable feeding in manual and automated MIG systems.
- Flexible Supply Options: Wire diameters, spool configurations, packaging, and order quantities can be reviewed according to customer equipment and production requirements.
- Quality Documentation: Material composition, inspection records, batch identification, and applicable compliance documents can be arranged according to individual order requirements.
- Production and Procurement Support: Chalco coordinates specification reviews, delivery requirements, and repeat-order planning for industrial welding projects.
Chalco supports welding wire quality through material verification, dimensional and surface inspection, and packaging checks. For repeat orders, customers can specify batch consistency, traceability, and documentation requirements to support their production and quality management processes.
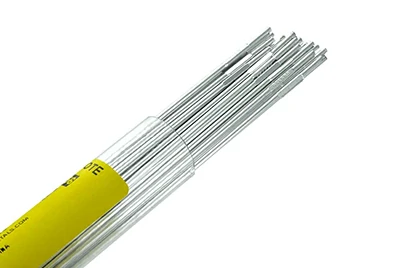
In addition to aluminum welding wire, Chalco can review requirements for compatible TIG filler rods and other aluminum joining materials. Product form and process suitability should be confirmed separately for each application.
Aluminum Welding Wire Buying Guide and FAQ
What is the difference between welding wire, welding rod and filler rod? Can they be used interchangeably?
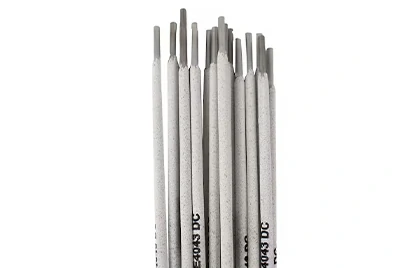
MIG welding wire, TIG filler rods, and aluminum stick welding electrodes are different types of aluminum joining consumables. Their feeding methods, electrode functions, and welding processes differ, so they should be selected according to the intended joining method rather than treated as interchangeable products:
| Name | Flux Coating | How to use | Functions as an Electrode? | Typical Applications |
| Welding Wire | No | Continuously fed electrode wire for MIG/GMAW; separate filler feed for suitable automated TIG/GTAW systems | Yes in MIG/GMAW | Industrial structure welding, high efficiency and continuous operation |
| Stick Welding Rod | Yes | Manual Metal Arc Welding (SMAW) | Yes in SMAW | Maintenance/field construction, where gas is not available |
| Filler Rod | No | Manually added filler metal in TIG/GTAW welding | No in TIG/GTAW | Precision welding, thin plates, small parts butt joint |
For other brazing welding product needs, please click [Aluminum filler rod][Aluminum welding and brazing materials] to view product details
Which Welding Wire Is Suitable for 6061 Aluminum?
In 6061 aluminum welding, ER4043, ER5356, and ER4943 may be evaluated according to joint strength, appearance, service conditions, and post-weld requirements. Final filler selection should follow the applicable welding specification.
Which welding wire should I choose when welding 5083 or 5052?
ER5356 and ER5183 are among the filler options that may be considered for compatible 5xxx aluminum alloy joints. Selection should account for the base alloy, magnesium content, service temperature, corrosion environment, and required weld properties.
How to choose welding wire diameter?
Usually selected according to the thickness of the parent material:
- <3mm: Use 0.8mm or 1.0mm
- 3–6mm: Use 1.2mm
- 6mm or thick plate welding: When using 1.6mm automatic welding/robot welding, it is recommended to use precision-wound large-diameter stable welding wire.
What wire packaging specifications does Chalco support?
Support 0.5kg / 1kg / 2kg / 5kg / 7kg / 15kg / 20kg / 250kg barrels. The reels can be made of plastic shaft, steel shaft or customized core.
Can you provide technical documents such as COA, MSDS, ROHS, etc.?
Documentation can be reviewed according to the welding wire grade, applicable specifications, and purchase order requirements. Depending on the product and agreed scope, supporting documents may include:
- COA (Composition Analysis)
- MSDS (Safety Data Sheet)
- RoHS/REACH (Environmental Compliance)
- Third-party test report (on demand)
Which wire feeders are compatible with Chalco aluminum welding wire?
- Universal MIG welding wire feeding system (Lincoln, Fronius, ESAB, OTC, etc.)
- Automated welding workstation, robotic welding arm
- TIG welding machine with wire feed module
Can you customize special alloys or wire specifications?
Of course. Chalco provides customized alloy development services, including composition fine-tuning, special ratios, composite structures, and non-standard wire diameter customization, supporting sample verification and batch supply.
Order Aluminum Welding Wire from Chalco
Looking for aluminum welding wire for industrial production or an upcoming welding project? Chalco supplies ER4043, ER5356, ER5183, ER4943, and other aluminum filler grades for suitable MIG and TIG applications, with specification and packaging options based on your purchasing requirements.
Send us your required alloy grade, wire diameter, spool size or packaging, order quantity, and destination. If you are unsure which filler metal to choose, you can also share your base aluminum alloy, welding process, and application requirements. Our team can help review suitable product options and prepare a quotation.
Chalco can provide you the most comprehensive inventory of aluminum products and can also supply you customized products. Precise quotation will be provided within 24 hours.
Get a quote